EN19 Alloy Steel Seamless Pipe
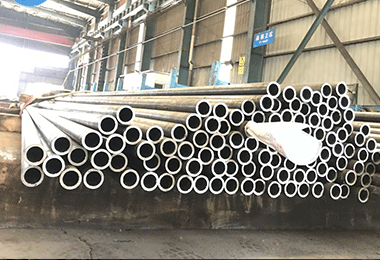
EN19 Alloy Steel Seamless Pipe is an alloy steel seamless pipe made of EN19 (also known as 42CrMo4 or 1.7225).
| Item | Value |
|---|---|
| Product | HFW (high-frequency welded) line pipe, externally coated |
| Standard & grade | API 5L, X52, PSL2 (L360 PSL2) |
| Size | 6 in (DN150) × 0.375 in — 168.3 mm OD × 9.53 mm WT |
| Total length | 5,508 m |
| Unit weight | 37.37 kg/m — total ≈205.8 t |
| Joints | ≈459 lengths at 12 m nominal (derived — confirm actual length) |
| External coating | Two systems: 3LPP 2.5 mm · FBE 400 µm |
| Coating cutback | Bare ends for field girth welding, dimensions recorded per length |
| Certification | EN 10204 3.1 mill certificate, heat-number traceable; coating report per length |
| Terms / delivery | CIF Alexandria, Egypt |
| PO accepted | September 27, 2026 |
The order of operations is fixed by physics and cannot be rearranged to save time. Once the pipe is coated, the weld seam can no longer be inspected by conventional non-destructive methods — an imperfection would be sealed under the jacket. So all mill testing precedes all coating:
| Step | Operation | Where |
|---|---|---|
| 1 | Coil forming, HFW welding, sizing and straightening | Pipe mill |
| 2 | Hydrostatic test, every length | Pipe mill |
| 3 | Full-length weld-seam NDT, plus body/edge checks | Pipe mill |
| 4 | Tensile, Charpy and chemistry per heat and per test unit | Mill laboratory |
| 5 | Dimensional check — OD, wall, ovality, length, square cut | Pipe mill |
| 6 | Grit blasting to the specified surface profile | Coating applicator |
| 7 | Coating application — FBE 400 µm and 3LPP 2.5 mm, separately | Coating applicator |
| 8 | Coating inspection — thickness, holiday test, adhesion | Coating applicator |
| 9 | Cutback to bare ends and final visual on every length | Coating applicator |
| 10 | Bundling, loading, CIF Alexandria | Tianjin Xingang |
Milestone dates for production and shipment are held on the order schedule and are not published here. If you are comparing suppliers, ask each one to state which steps happen at which plant — a quote that lists coating and mill testing as a single line has not separated the two.
The two systems solve different problems on the same pipeline. Fusion bonded epoxy (FBE) at 400 µm is the standard anti-corrosion coating for buried line pipe in benign soil at moderate operating temperature. Three-layer polypropylene (3LPP) at 2.5 mm adds a thick polypropylene jacket over an FBE primer and an adhesive layer, giving mechanical protection against rocky backfill, crossings and higher operating temperature. Specifying both means the buyer has split the line into sections — usually FBE for the main run, 3LPP for the demanding sections.
Cutback is the bare steel length left uncoated at each pipe end — typically 100 to 150 mm — so that field girth welds can be made without burning or damaging the coating. If the cutback is short or uneven, the welding heat damages the coating edge and the field joint sleeve cannot be applied correctly; if it is too long, the joint becomes an unprotected corrosion window. Cutback dimensions are measured and recorded by the coating applicator on every length.
Always after. Hydrostatic testing and full-length weld-seam non-destructive examination are completed at the pipe mill, because once the pipe is coated the weld seam can no longer be inspected by conventional means and any imperfection is sealed under the coating. The order of operations is: forming and welding, hydrostatic test, weld-seam NDT, dimensional check, grit blasting, then coating, then cutback and final visual.
A coated line pipe order spans two plants — the pipe mill and the coating applicator — plus third-party inspection and ocean freight. A trading supplier selects the mill whose size range and PSL2 capability fit the specification, nominates a coating applicator qualified for the coating system ordered, moves the pipe between the two plants without surface damage, keeps heat numbers matched to coating batch records, arranges inspection at both sites, and consolidates the mill certificate, coating report and shipping documents into one traceable set under a single bill of lading. A single mill can only supply what it rolls, in the coating it applies.